Category: Uncategorized
One-piece pinions for high-speed applications
18 August, 2026
At high rotational speeds, geometry tolerance is everything. Especially in one-piece pinions, where there is no later assembly step to correct errors or compensate for small deviations. The shaft and gear are one solid component, so the accuracy has to be built directly into the machining process.
That is what makes complex one-piece pinions technically demanding. Two elements are especially critical:
- Minimal run-out towards the thrust faces
- Precise positioning of the toothing in a confined geometry.
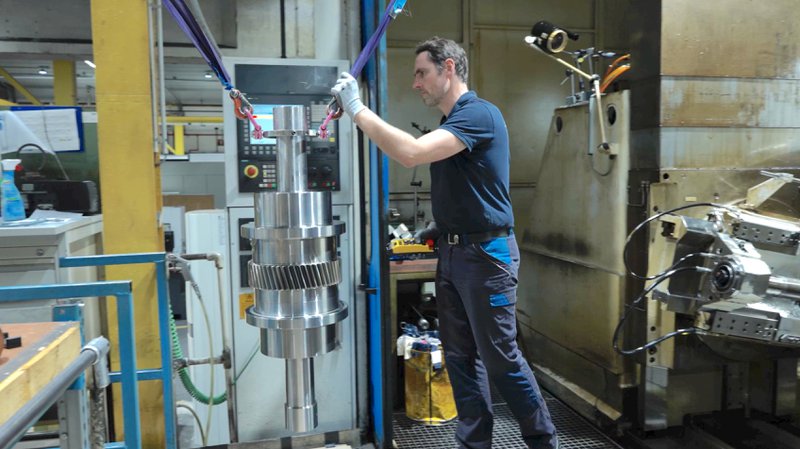
1. Minimal run-out towards the thrust faces in one-piece pinions
In high-speed applications, the transition between the toothing and the thrust faces is critical.
A very small axial run-out means the gear teeth are positioned extremely close to the thrust surfaces. This limits design freedom during machining, increases sensitivity to deflection and tool access, and leaves very little margin for error.
Maintaining accuracy here requires:
- highly stable fixturing
- precise alignment of datum references
- full control over cutting forces during gear generation
In one-piece pinions, this is even more important because the gear teeth, shaft and thrust faces all belong to the same component. One small deviation can influence the final running behaviour.
2. Precise toothing position in complex one-piece pinions
When the toothing sits compactly between functional faces, tooth generation becomes significantly more complex.
The tighter everything is packed, the more difficult it becomes to achieve:
- correct tooth flank geometry
- consistent lead and profile
- proper finish without damaging adjacent surfaces
This is where experience, machine capability and process control come together.
For one-piece pinions, precise tooth positioning is not only about cutting the teeth correctly. It is about maintaining the full relationship between the toothing, shaft and functional surfaces.
Gear tooth generation
In the video, you see one crucial step of that process: gear tooth generation.
The process starts with accurate mounting of the blank. From there, controlled cutting, inspection and initial deburring help ensure that the required geometry is achieved before the part moves further in the process. One solid part. Very tight tolerances. A process designed around complexity. That is what enables reliable one-piece pinions for demanding, high-speed applications.
Talk to us about your pinion project
Do you have a high-speed application where geometry, run-out and process stability are critical?
Our team can support you from feasibility to production, with practical input on design, manufacturability and process control.
Contact our sales team via sales@igwpower.com or reach out through our contact page.
Micron-level tolerances at IGW: maintaining precision even on large components
15 July, 2026
At IGW, precision is measured in microns. We strive for micron-level tolerances through every step of production. On one project, our team achieved a tolerance of 15 microns on a gear with a diameter of around 2 metres.
What does a micron-level tolerance mean?
A micron is one thousandth of a millimetre. So 15 microns equals 0.015 mm. To make that more understandable, 15 microns is in the range of a thin sheet of kitchen aluminium foil. It is also much thinner than a human hair.

Why 15 microns is difficult on a 2-metre gear
A micron-level tolerance with a large steel component depends on temperatures too.
Steel expands when temperature changes. As a practical rule of thumb, steel expands by roughly 12 microns per metre per degree Celsius. On a 2-metre gear, a temperature change of just 1°C can already create around 24 microns of dimensional change.
That is more than the 15-micron tolerance itself. This is why precision gear manufacturing depends on more than machine capability. Temperature, clamping, tool behaviour, machine stability and measurement conditions all influence the final result.
Precision is measured throughout the process
For tolerances like this, measurement is not something that only happens at the end.
Critical features are checked during the process, so the team can verify whether machining remains stable and within the required limits. Final inspection is still essential, but it confirms the result of a controlled process. A 15-micron tolerance on a 2-metre gear is only possible when machining and metrology work together from the start.

What micron-level gear tolerances mean for customers
For customers, tolerances are not just numbers on a drawing. They determine how a gear fits, runs and performs inside demanding rotating equipment. When geometry is controlled at micron level, it supports accurate assembly, stable operation and reliable performance over time.
At IGW, achieving micron-level tolerances is the result of stable machining, controlled conditions and experienced people who understand how small deviations can affect large components. That is where precision becomes repeatable.
That is why micron-level tolerances have to be built into the process.
Talk to us about precision manufacturing
Do you have a project where tight tolerances, stable machining and reliable measurement are critical?
We machine gears with a diameter of up to 2,3 meters. Our team can support you from feasibility to production, with practical input on geometry, process control and manufacturability.
Contact our sales team via sales@igwpower.com or get in touch through our contact page.
Large gear manufacturing at IGW: our biggest gear yet
25 June, 2026
At IGW, large gear manufacturing is not a marketing claim. It is a practical capability, proven on the shopfloor. We machine gearwheels up to Ø 2.3 m as part of our industrial gear offering, supporting customers who need high torque, reliable performance and controlled geometry at scale.
Recently, we reached a new internal milestone: the largest gear ever produced within IGW, with a diameter of Ø 2.2 m. Before this project, we had already delivered Ø 2.0 m gears. This time, the extra 200 mm mattered. Not only for machining and inspection, but also for something more basic and just as critical: moving the part safely through the building.

Why a Ø 2.2 m gear changes the process
When gear diameter increases, standard assumptions quickly stop being reliable.
A few extra centimetres can affect the machine envelope, clamping strategy, tool approach, inspection setup and internal logistics. Cranes, turning devices, transport routes, floor load, turning radius and door clearance all become part of the manufacturing plan.
Large gear manufacturing is rarely only a machining challenge. It is a complete process challenge: planning, execution, verification and handling. Each step needs the same discipline as the cutting operation itself.
At IGW, that end-to-end mindset is part of how we work. By keeping key steps in-house, we maintain control over the process, reduce uncertainty and support predictable outcomes.

The measuring stick that protected the schedule
For this project, our team introduced a simple but effective tool: a dedicated measuring stick representing the critical outer dimensions of the gear and its handling setup.
Why a physical measuring stick?
Because in real production environments, the tightest constraint is not always the machine. It can be the route between stations. The turning area, crane travel corridor, staging zones and doorways can all become critical.
The measuring stick helped us validate early and repeatedly that:
- the gear would fit the machining setup as planned
- the gear could be moved safely between operations
- the gear could pass through every doorway and bottleneck
- no last-minute rework, disassembly or unnecessary risk would be introduced
The result was fewer surprises, clearer internal communication and a smoother path toward first-time-right execution.
What customers gain from proven large gear capability
When sourcing a gear of this size, customers need predictable delivery and verified performance. The goal is not heroic problem-solving near the deadline. The goal is a controlled process from the start.
IGW supports large gear projects with:
- controlled geometry and verification for demanding industrial requirements
- in-house process control across key manufacturing steps
- the ability to manufacture large gearwheels up to Ø 2.3 m
- practical expertise in handling, inspection and integration
- a global manufacturing footprint to support customers worldwide
For machinery where uptime matters, these details translate into fewer delays, fewer deviations and more confidence during commissioning.
Let’s talk about your large gear project
If you are considering a gear in the Ø 2.0 to Ø 2.3 m range, or if you are not sure what is feasible within your assembly constraints, IGW can support you from feasibility through delivery.
Our team combines large gear manufacturing expertise with practical input on handling, inspection and integration.
Learn more about our gear capabilities on our website.
Reach out to our team: sales@igwpower.com
Learning through cross-site training
2 April, 2026
In precision manufacturing, consistent results do not come from machines alone. They come from shared standards, repeatable routines, and people who understand every step of the process.
In January 2026, IGW Romania hosted colleagues from VCST Mexico, IGW India and IGW China for a hands-on technical training and integration program. The goal was clear. Align expertise across sites, deepen process understanding, and strengthen collaboration through real shopfloor work.


Why cross-site training matters at IGW
When multiple sites support similar technologies and customers, consistency becomes a daily discipline. Cross-site training helps teams:
- Transfer practical know-how faster than documentation alone ever can
- Align process thinking and quality expectations across regions
- Build a shared language between engineering, production and inspection
- Reduce ramp-up time on new processes and equipment
This is how IGW builds capability at scale, without losing control of quality.
One month of sharing knowledge
Throughout the month, specialists from several technical domains joined IGW Romania’s teams, including process engineering, product engineering, CNC programming, operations and quality control.
Deep dive with IGW China
The month started with a visit from Nick Liu, Process Specialist from IGW China, focusing on the gear grinding process on the Viper500. The program also covered complementary steps such as part balancing and assembly, where precision is not optional and process understanding is critical.

Knowledge exchange with VCST Mexico
IGW Romania welcomed colleagues from VCST Mexico, covering multiple roles and viewpoints:
- Martin Posada, Project Leader
- Miguel Castillo, CNC Programmer with expertise in hobbing and gear grinding
- Victor Salazar, CTX Gamma Operator and Setter
- Carlos Perez and Jose Mares, Quality Inspectors
Their focus included production flows and key operations on the DMG Gamma machine, combined with best-practice exchange on how processes are organised and controlled on the shopfloor.

Workflow immersion with IGW India
From IGW India, Tanmay Guldagad and Komal Giram, Product Engineers, followed the full manufacturing route end to end. Turning, milling, hobbing, grinding, and dimensional inspection. They also participated in evaluating tools and measuring equipment, reinforcing what each step requires in terms of preparation, stability and verification.
What this strengthens
By working directly with operations and technical teams, participants gained an in-depth view of how IGW Romania structures production and maintains strict quality standards. The impact goes beyond training. It strengthens the foundation of a global organisation built on:
- Shared ways of working
- Comparable technical judgement across sites
- Collaboration that is practical, not theoretical
- Continuous learning embedded in daily operations
Looking ahead
IGW remains committed to developing people and supporting the growth of specialists through real technical training, access to modern technologies, and collaboration across borders. Initiatives like this build a stronger global team, united by shared standards and a clear focus on performance.
Expanding our large machined component capabilities in Oostkamp
30 March, 2026
At IGW, continuous improvement in production is driven by long-term preparation, not quick wins. The recent installation of a Starrag STC1600 at our Oostkamp site is a clear example of that approach.
This new machine strengthens our capabilities in high-precision, large machined components, while increasing process stability and future capacity.
A project built over time
The Starrag STC1600 project started in June 2023. From the beginning, the focus went far beyond installing a machine. The objective was to deliver a fully integrated production solution that fits seamlessly into our existing processes.
The physical installation on site took approximately six weeks. However, the largest effort was dedicated to developing the turn-key setup.
In this context, turn-key means that the machine was delivered as a complete, production-ready system. This includes machine configuration, probing strategies, clamping concepts and process validation. When the machine entered production, it was ready to run according to IGW standards, not requiring further fundamental development.

The Starrag STC1600 is a 5-axis milling machine dedicated to large machined components with high precision. A key feature is the use of hydraulic clamping, supported by custom-developed fixtures.
These hydraulic fixtures were specifically designed for IGW’s components and required significant development time. Their role is to ensure repeatable positioning, stable machining conditions and consistent quality throughout long machining cycles.
Although the machine is currently used for two specific component types, its technical capabilities allow for a much broader application range in the future.
Key machine characteristics:
- 5-axis milling for large components
- Hydraulic clamping with custom fixtures
- Spindle speed up to 12,000 RPM
- Tool magazine with a capacity of 220 slots

A multidisciplinary effort
Bringing the Starrag STC1600 into production was a collaborative effort across multiple teams.
Around 15 colleagues within IGW were involved, in the installation. In addition, software specialists supported the development of post-processors and digital integration, ensuring reliable and repeatable machining programs from day one.
This cross-functional approach ensured that the machine was not only installed, but fully embedded into IGW’s production environment.
Strengthening future capacity
The Starrag STC1600 represents more than an equipment upgrade. It reinforces IGW’s ability in large machined components with high precision, stable processes and controlled quality.
By investing in both technology and process development, IGW continues to prepare its manufacturing operations for increasing complexity and future customer requirements.
Curious what we manufacture on this machine today?
The Starrag STC1600 is currently used for two specific, large machined components. 👉 Discover more about our capabilities here: https://igwpower.com/large-machined-components/
Do you have large machined components that require high precision and controlled processes?
Feel free to reach out to our team at sales@igwpower.com.
IGW India certifies 20 new Lean Six Sigma Green Belts
30 March, 2026
We’re proud to announce that 20 team members at IGW India have earned their Lean Six Sigma Green Belt certification. This is a significant step forward in our ongoing focus on building smarter systems, improving quality, and developing skilled, future-ready talent.
With this certification, these employees are now equipped to lead improvement projects across the organization. This makes processes more efficient, more consistent, and more customer-focused.
But what exactly is Lean Six Sigma, and why does it matter?
What is Lean Six Sigma?
Lean Six Sigma is a widely adopted method used by companies around the world to improve how work gets done. It combines two proven approaches:
- Lean is all about removing unnecessary steps, cutting down delays, and streamlining workflows.
- Six Sigma focuses on reducing errors, improving quality, and using data to guide decisions.
Together, they offer a structured way to solve problems and create lasting improvements in everything from manufacturing and logistics to customer service and product development.
Why is Lean Six Sigma relevant for modern companies?
In competitive industries (whether it’s manufacturing, healthcare, IT, or finance), delays, inefficiencies, and errors can quickly pile up and impact performance. Lean Six Sigma helps organizations take a step back and look at how things are working (or not working), then apply a clear, data-driven method to improve them.
The result? Better quality, faster delivery, happier customers, and more efficient use of time and resources.
Lean Six Sigma at IGW
We manufacture precision gear systems used in critical applications across transportation, energy, and industry. That means every detail matters; from the accuracy of a gear tooth to the timing of a delivery.
By embedding Lean Six Sigma principles into our daily work, we’re able to:
- Spot and eliminate inefficiencies before they grow into bigger issues
- Standardize best practices across teams and shifts
- Improve product quality and reduce scrap
- Speed up lead times without cutting corners
- Build a stronger, more agile organization
It’s not just about fixing problems when they happen. It’s about building systems that prevent them from happening in the first place.

Is Lean Six Sigma better than other methods?
What sets Lean Six Sigma apart is its blend of logic and practicality. While many improvement methods rely on broad strategies or one-size-fits-all solutions, Lean Six Sigma gives teams concrete tools to analyze what's really happening, find the root causes of problems, and implement solutions that stick.
It also creates a common language across departments. Whether someone works in engineering, operations, or customer support; Lean Six Sigma provides a shared structure for problem-solving based on data, not guesswork.
Is it difficult to earn a green belt?
Earning a Lean Six Sigma Green Belt isn’t something you do in a weekend. It requires focused training in key concepts like process mapping, root cause analysis, and statistical thinking. It also involves completing a real-world project that shows the candidate can turn theory into action.
That’s why Green Belt certification is widely respected. It reflects not just knowledge, but the ability to improve real systems in meaningful ways.

What does this mean for IGW India?
We see this certification as more than a personal achievement. It’s an investment in how we work as a team. Our newly certified Green Belts will now take the lead on identifying inefficiencies, improving workflows, and helping us deliver better results for customers and colleagues alike.
Congratulations to the 20 team members who’ve stepped into this new role. We’re excited to see where your skills take us next.
Compressed air, big impact: What a compressor actually does
30 March, 2026
You’ve probably heard the word compressor thrown around in industrial settings, or maybe in the context of your air conditioning or car. But what is a compressor, really—and why do so many industries rely on them?
Let’s break it down and uncover the difference between two major players in the compressor world: rotary and centrifugal compressors.
So… What’s a compressor?
Think of a compressor like a super-strong lung. Its job is to take in gas—usually air—and squeeze it, increasing the pressure while shrinking the volume. That compressed air is then used to do all kinds of work: powering tools, cooling buildings, moving gas through pipelines… the list goes on.
Basically, if it hisses, spins, cools, or lifts—there’s a good chance a compressor is involved.
Where do you find compressors?
Everywhere. Seriously.
- factories: Running machinery and powering pneumatic tools. Compressors are used to produce clean air which is necessary to produce for example microchips through semi-conductors.
- Oil & Gas: Moving natural gas through pipelines
- HVAC systems: Helping your fridge or AC keep things chill
- Power plants: Supporting turbines and energy production
- Transport: In air brakes, turbochargers, and even airplane systems, reconvert gases released over time from LNG back into LNG, to power ships with gas engines for example.
Different jobs call for different kinds of compressors—and that's where things get interesting.
The compressor showdown: Rotary vs. Centrifugal
Not all compressors are created equal. Let’s meet our two main contenders:
Rotary Compressors – The Reliable Workhorse
These guys use rotating screws, vanes, or lobes to do the squeezing. They're tough, compact, and great at working steadily without fuss.
Why people love them:
- Quiet and compact
- Perfect for constant use
- Low maintenance = fewer headaches
- Ideal for medium pressure jobs (think factories or workshops)
🔧 Best used for: Day-in, day-out tasks where durability and reliability matter more than speed or scale.

Centrifugal compressors – The high-speed performer
Instead of squeezing gas between screws, centrifugal compressors spin it like crazy. A fast-moving impeller flings gas outward, building pressure as it slows in a diffuser.
Why they’re cool:
- High flow, high pressure = big power
- Excellent energy efficiency at large scales
- Often oil-free, which is great for cleanliness and maintenance
- Great for continuous operation in massive setups
🏭 Best used for: Large industrial plants, gas pipelines, chemical processing—basically, the big leagues.

Which one’s right for you?
Here’s a quick cheat sheet:
| You Need… | Go With… |
|---|---|
| Reliable pressure in a compact setup | Rotary compressor |
| High-speed airflow for massive systems | Centrifugal compressor |
| Lower upfront cost and easy upkeep | Rotary |
| Energy efficiency at scale | Centrifugal |
And what does IGW have to do with it?
Well, compressors don’t run on magic—they run on precision gears. And that’s where we come in.
At IGW, we craft top-quality gears that keep compressors running smoothly, quietly, and efficiently. Whether you're working with a rugged rotary system or a high-performance centrifugal setup, our gears are built to deliver power without compromise.
So the next time you hear the hiss of compressed air or the hum of a spinning machine, think of the gears making it all happen. That’s us.
IGW India scores Diamond Award at iNFHRA Awards 2025
30 March, 2026
We’re beyond excited to share that IGW India has taken home the Diamond Award in the “Tech-Driven Workplace Change” category at the Corporate Excellence Awards 2025 by iNFHRA!
This top honor celebrates our bold approach to innovation, our ongoing drive for sustainability, and the smart solutions we’re bringing to life on the shop floor every day.
What are the iNFHRA Awards?
Hosted annually by the Infrastructure, Facility, Human Resource & Realty Association (iNFHRA), the iNFHRA Awards spotlight organizations across India that are shaking up the workplace industry — from cutting-edge technology and intelligent infrastructure to ambitious sustainability efforts and people-first HR initiatives.
In other words, these awards don’t just recognize operational success — they celebrate transformational impact. Companies that are making a difference not just for their bottom line, but for their people, their communities, and the planet.
That’s exactly why winning the Diamond Award — the highest honor in our category — means so much. It’s a powerful acknowledgment of how we’re using technology to make real, measurable improvements on the shop floor and beyond.
Recognizing our achievements in innovation and sustainability
At IGW India, we believe that innovation is only meaningful when it delivers real-world results. That’s why we’ve invested in forward-thinking solutions like diagonal hobbing technology, which enhances gear production efficiency, and solar energy integration, which helps us dramatically reduce our carbon footprint.
Together, these initiatives reflect our commitment to building a smarter, greener, and more future-ready manufacturing environment.
Fittingly, this prestigious award was accepted at the iNFHRA Awards ceremony by our very own Mr. Vikas Dudeja (Plant Manager) and Mr. Sandip Mali (Engineering Manager) — a proud and defining moment for all of us at IGW India.
A team effort worth celebrating
Of course, none of this would have been possible without the incredible teamwork behind it.
This isn’t just a win for IGW India — it’s a celebration of all the individuals who make our organization what it is. From the shop floor to senior leadership, it’s your passion, creativity, and dedication that turned bold ideas into reality.
Whether you’re solving complex technical challenges or driving excellence in day-to-day operations, your efforts made this recognition possible.
Looking ahead
As we take a moment to celebrate this achievement, our eyes are firmly set on the road ahead.
We’ll continue to innovate, collaborate, and lead the charge toward a more sustainable, efficient, and tech-driven manufacturing future.
A heartfelt thank you to the entire IGW India team — this Diamond Award is yours. Let’s keep reaching higher, together.
IGW’s expertise in large machined components supports world‑leading industries
, 30 March, 2026
While gears are at the origin of IGW, our capabilities extend far beyond drivetrain technology. For more than 50 years, we have built deep expertise in the manufacturing of large machined components, enabling us to serve customers who rely on extreme precision, reliability, and flawless execution.
Today, our components are used in highly demanding sectors, including medical technology and semiconductor lithography, yet our capabilities extend far beyond these applications.
Supporting critical healthcare technology
One of our long‑standing customers is a global leader in healthcare technology. For their advanced imaging equipment, we deliver large machined components used in scanners that support medical personnel during interventional X‑ray procedures. What sets IGW apart is our ability to deliver fully finished, assembly‑ready parts. The process starts with castings delivered to our Oostkamp facility. From there, we manage the complete transformation—from machining to inspection, painting, and final finishing, so the components arrive at the customer completely ready for integration into their systems.

In the semiconductor lithography sector, the standards for quality are incomparable. Machines used in this field must achieve accuracy measured in nanometres, requirements that leave no room for compromise. We are proud to manufacture large machined components for a world‑leading OEM in this industry. These include one of the structural frames used in sophisticated lithography systems that power the production of advanced electronic components worldwide. Just as in our medical projects, we manage the entire supply chain, from rough material to the final finished part. Our scope includes machining, surface treatment, and sub‑assembly performed in a controlled clean‑area environment before shipment to the customer.

Large machined components present unique engineering challenges. Their size introduces potential variations, such as deformation throughout the production process, which require absolute control and deep technical experience. Thanks to more than three decades of expertise, our teams have developed the know‑how to consistently deliver reliable, high‑precision components, built to perform in the most demanding applications and environments.
Proud of the trust placed in us
We are honoured that global industry leaders rely on our components for critical applications across multiple markets. While medical technology and semiconductor manufacturing are strong examples of where our parts are used today, our expertise is not limited to these sectors. IGW continues to expand its capabilities to support a broad range of industries that require complex, high‑quality large machined components. Driven by the trust of our customers, we look forward to embracing new challenges and continuing our journey of precision manufacturing excellence.
IGW accelerates production capabilities with new MCM machining center
, 30 March, 2026
Despite challenging market conditions, IGW continues to grow and invest in the future. One of our latest milestones is the installation of a brand‑new MCM machining center—an important step that strengthens our capacity for large machined components and supports our long‑term strategic ambition to deliver faster, smarter, and more flexible manufacturing solutions.
A future‑proof investment in efficiency and innovation
The investment was driven by two major developments:
- an increasing demand for new and complex components, and
- emerging technologies that significantly enhance manufacturing speed, reliability, and efficiency.
The new MCM machine replaces a 20‑year‑old unit and is expected to serve at least two more decades. More importantly, it introduces a new level of automation and precision to our machining operations.
https://www.youtube.com/watch?v=jKjqj5-27_Q
Higher capacity, greater flexibility
Equipped with a robotic deburring cell and state‑of‑the‑art 5‑axis machining centers connected via automated pallet pools, the new MCM line significantly boosts our production capabilities.
These innovations allow us to:
- shorten our time‑to‑market
- increase throughput and production stability
- react more flexibly to customer needs
This 2‑million‑euro investment is already proving to be a smart move. With demand continuing to rise, IGW is currently evaluating the purchase of two additional machines dedicated to smaller components.
Enabling precision across diverse industries
The new machining center is used for the production of IGW’s high‑quality large machined components, ranging from 1 to 3 meters in aluminum.
Today, we manufacture parts for sectors such as:
- the medical industry (e.g., C‑arm components)
- global market‑leading OEMs in the semiconductor sector
These markets are examples of where our components are used today, but we are not limited to these sectors.
IGW’s advanced machining capabilities are designed to serve a broad and evolving range of industries where precision, reliability, and large‑scale aluminum components are essential.